16 Processes|Titanium Bike Frames, Titanium Machined Parts, Titanium Racks)
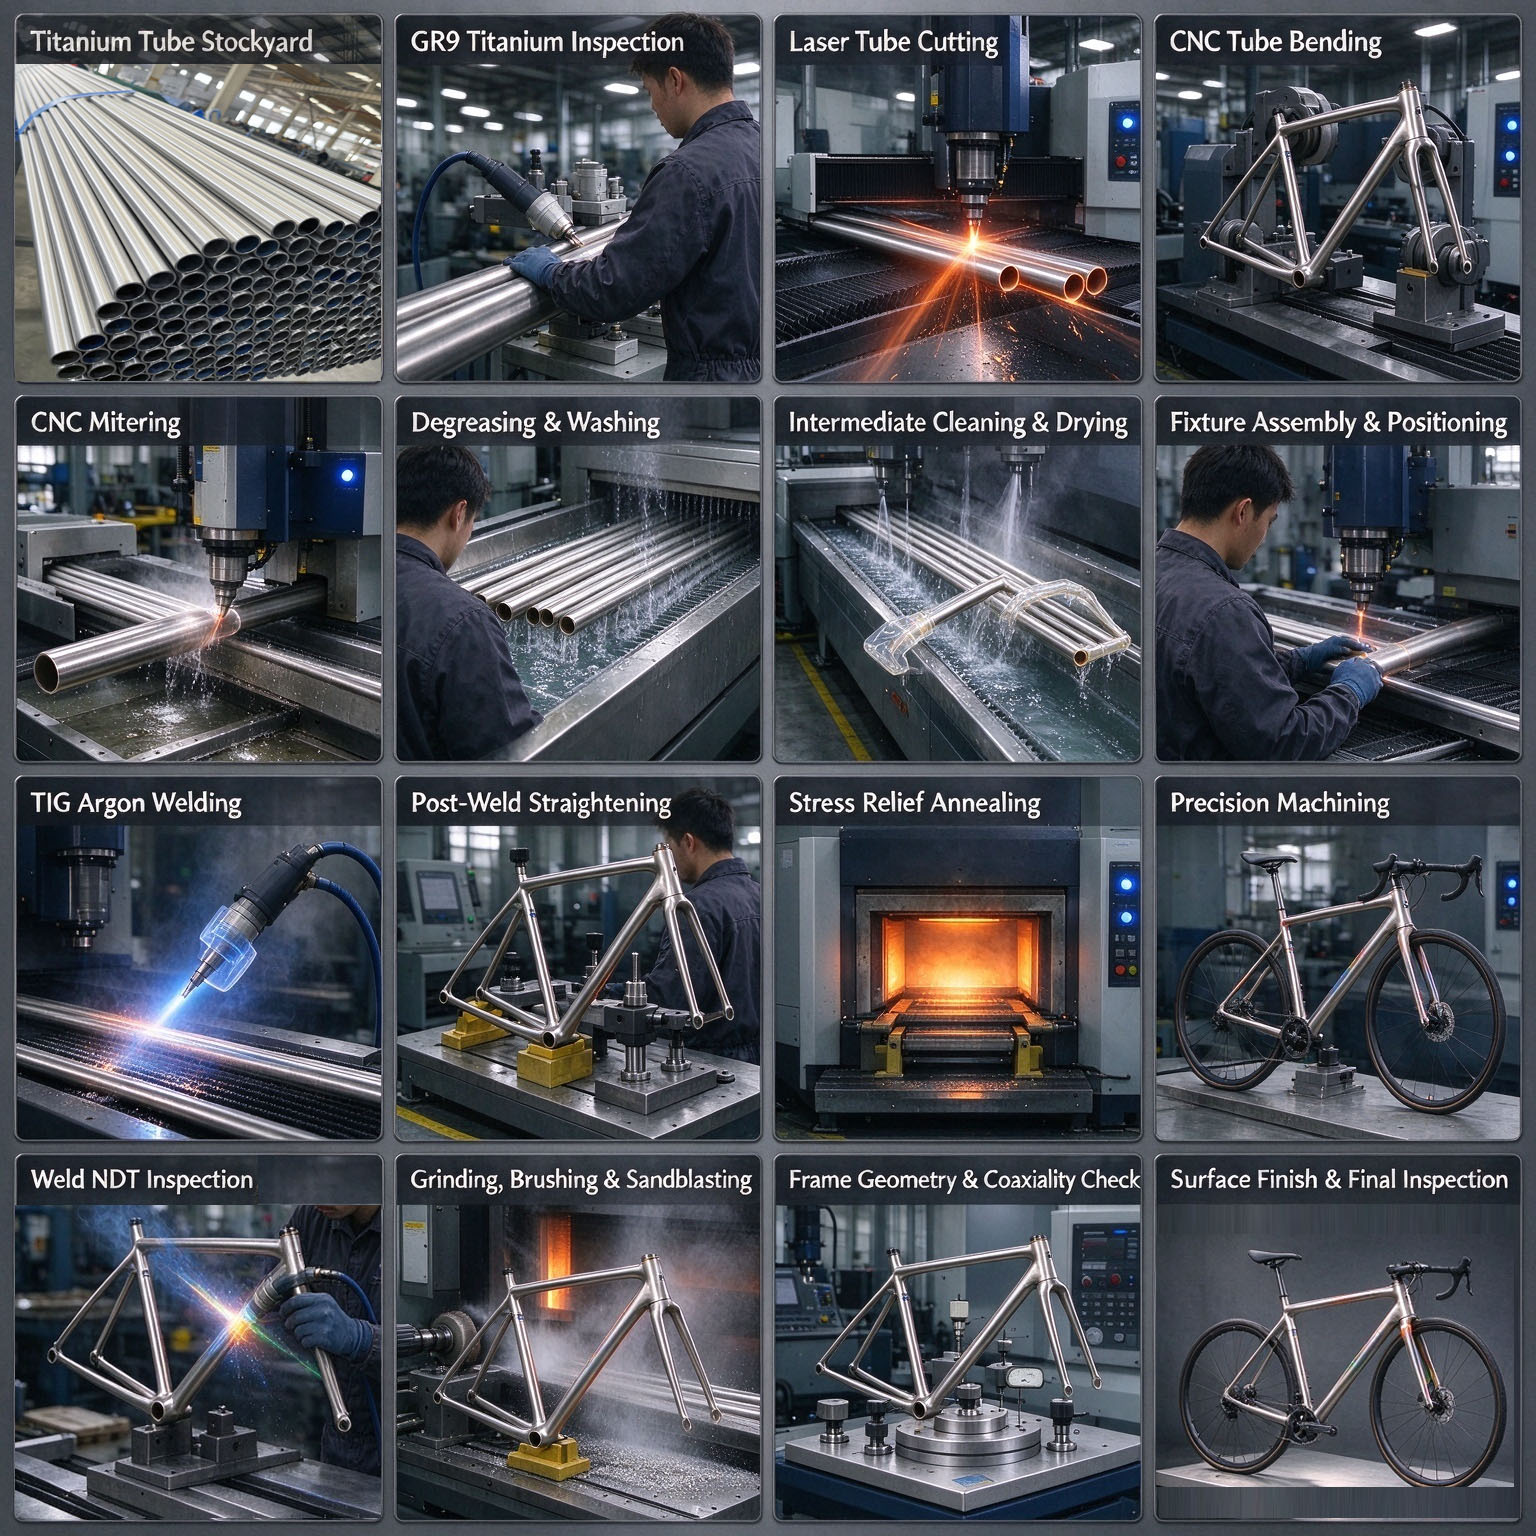
1.Raw Titanium Material Inspection & Warehousing
GR9 titanium tubes, rods and sheets are received. We verify material certificates, inspect surface condition and sample dimensions, to ensure the titanium stock has intact metallic luster without scratches, cracks or oxidation.
2.Laser Cutting & Blanking
Laser tube cutting machines cut titanium tubes and profiles precisely according to engineering drawings, producing raw tube blanks and sheet blanks.
3.CNC Tube Bending Forming
CNC benders bend titanium tubes to form curved frame tubes and rack tubes. Bending radius is strictly controlled to avoid wrinkling or cracking of titanium material.
4.CNC Miter & Intersection Groove Machining
CNC milling machines cut matching miter joints for tube connections. The fitting gap is controlled tightly to meet precision requirements for assembly and welding.
5.Degreasing & Cleaning
Titanium parts are cleaned in ultrasonic or immersion cleaning tanks to remove grease, cutting fluid and fingerprints, then dried thoroughly to prevent welding porosity and contamination.
6.Intermediate Rinsing & Drying
Clean water rinses away residual detergent. Hot air drying ensures no chemical residue remains on titanium surfaces.
7.Fixture Jig Assembly & Positioning
Titanium frame tubes, rack tubes and auxiliary fittings are mounted and positioned on custom welding jigs. Geometry and angles are aligned before tack welding.
8.TIG Argon Shielded Welding
Specialized pulsed TIG welding for titanium. Backside argon shielding inside tubes plus front-side gas protection are applied. Heat input is limited to prevent titanium embrittlement from absorbing hydrogen, oxygen and nitrogen; qualified welds show bright silver color.
9.Post-weld Straightening & Correction
Welded frames and racks are corrected on jigs with dial indicators. Welding distortion is adjusted to keep parallelism and form tolerance within drawing limits.
10.Vacuum Stress-relief Annealing
Workpieces are heated in vacuum or argon-protected furnaces at 500–550℃ to release welding residual stress and prevent later deformation or cracking.
11.Precision CNC Machining
CNC machining centers and turn-mill equipment complete finishing work: head tube facing & reaming, bottom bracket tapping & reaming, dropout machining, rack mount base and cable routing groove processing.
12.Non-destructive Weld Inspection (NDT)
Liquid penetrant inspection (FPI) is standard. X-ray RT inspection is available for high-end orders to detect tiny cracks, lack of fusion and hidden porosity inside welds.
13.Grinding, Brushing & Sandblasting Surface Treatment
Weld beads are ground and blended. Surface brushing creates fine metal grain texture; sandblasting delivers uniform matte titanium finish as selected.
14.Geometry & Coaxiality Measurement
Frames and racks are checked on dedicated inspection benches. We test bottom bracket coaxiality, rear dropout parallelism and all mounting datum dimensions.
15.Passivation, Laser Marking & Optional Anodizing
Titanium passivation improves corrosion resistance. Laser marking adds permanent logos or codes. Color anodizing is optional for decorative surface effects.
16.Final Finished Product Inspection
Full visual check, dimensional re-inspection and sampling fatigue testing. Qualified products are finished titanium bike frames, titanium racks and titanium bicycle components.
✅ Custom orders for titanium frames, titanium racks and all kinds of titanium bicycle machined parts are welcome!